栏目:产品应用·工艺深度 | 出品:东莞市凯立兴新材料科技有限公司(TPU 薄膜工厂) 说明:本文为无缝运动鞋鞋面、越野跑鞋支撑片、飞织鞋面补强及鞋带孔热贴高低温 TPU 膜应用与热压工程方法论科普,具体高低温层厚度配比、模具热压温度与剥离强度参数请以双方技术协议(TDS)与现场打样实测为准。
导语:从“针车缝合”到“热压无缝”,现代跑鞋的工艺革命
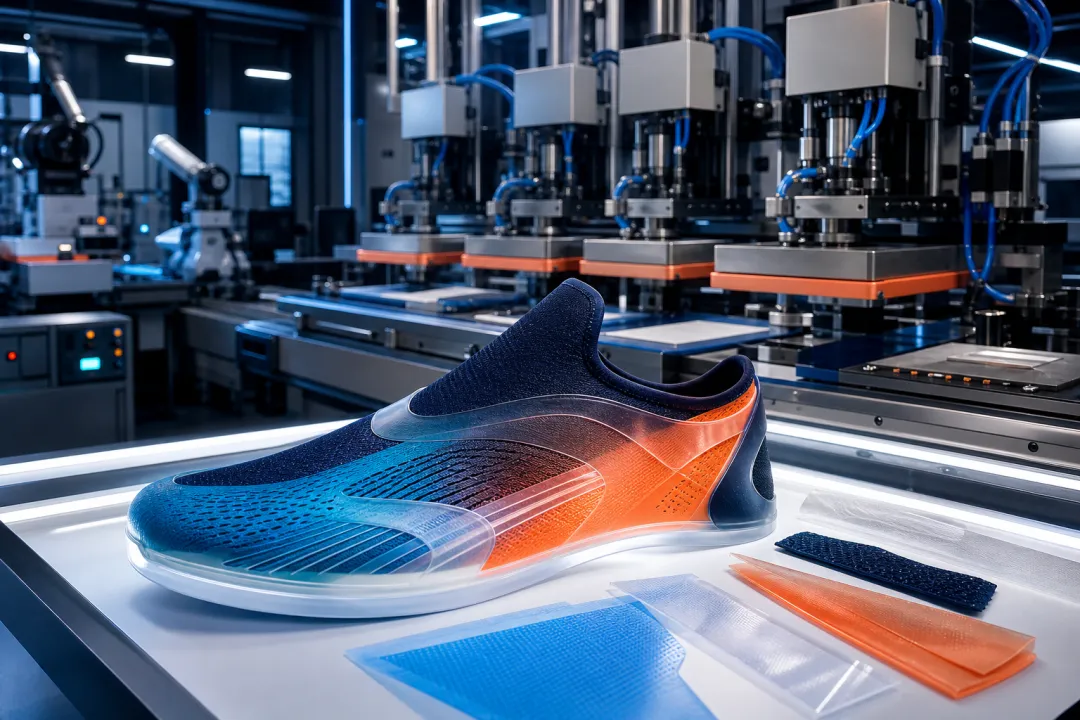
走在现代运动鞋代工厂的车间里,最直观的变革莫过于:过去排满数百台缝纫机的传统针车车间正在被全自动数控裁断机、高精度热压机与高频熔接产线全面取代。
在耐克、阿迪达斯、安踏、李宁等主流跑鞋、足球鞋、篮球鞋及户外越野鞋的鞋面上,传统厚重、易磨脚、且工序繁琐的车缝皮革裁片几乎消失不见,取而代之的是极致轻量、流线科技感十足、且支撑强韧的“无车缝热贴鞋面(Seamless No-Sew Upper)”。
实现这种“天衣无缝”美学与力学性能的核心材料,正是鞋材领域的王牌产品——高低温双层共挤 TPU 薄膜(High-Low Temperature Co-extruded TPU Film)。
很多鞋厂在采购与热压试样时常常踩坑:
为什么单层 TPU 膜一烫就全化掉、表面发粘变形?
为什么有些高低温膜压完后边缘溢胶严重,甚至把表层防粘离型纸也粘死?
为什么折弯 2 万次后,鞋头受力弯折区边缘直接起翘脱层?
今天这篇工艺深度干货,东莞市凯立兴新材料科技有限公司为你彻底讲透:高低温 TPU 膜的底层材料架构是什么?如何精准设定热压三要素?大货生产如何彻底杜绝溢胶与脱层?
一、材料本质:什么是“高低温”双层共挤 TPU 膜?
很多刚接触无缝鞋材的采购人员会问:既然都是 TPU,为什么不能直接用普通的单层热熔胶膜或单层高弹性膜?
如果用单层纯热熔胶膜(低熔点 80℃~100℃)
:热压时整张膜全部熔化变成液体胶水,不仅无法保留表面设计纹理、颜色与厚度,而且表面会严重粘模、污染热压头;
如果用单层高熔点 TPU 膜(高熔点 160℃~180℃)
:表面耐温耐磨了,但由于熔点太高,根本无法在鞋面织物纤维能承受的温度下软化渗透,热压后完全没有粘接力(一揭就脱)。
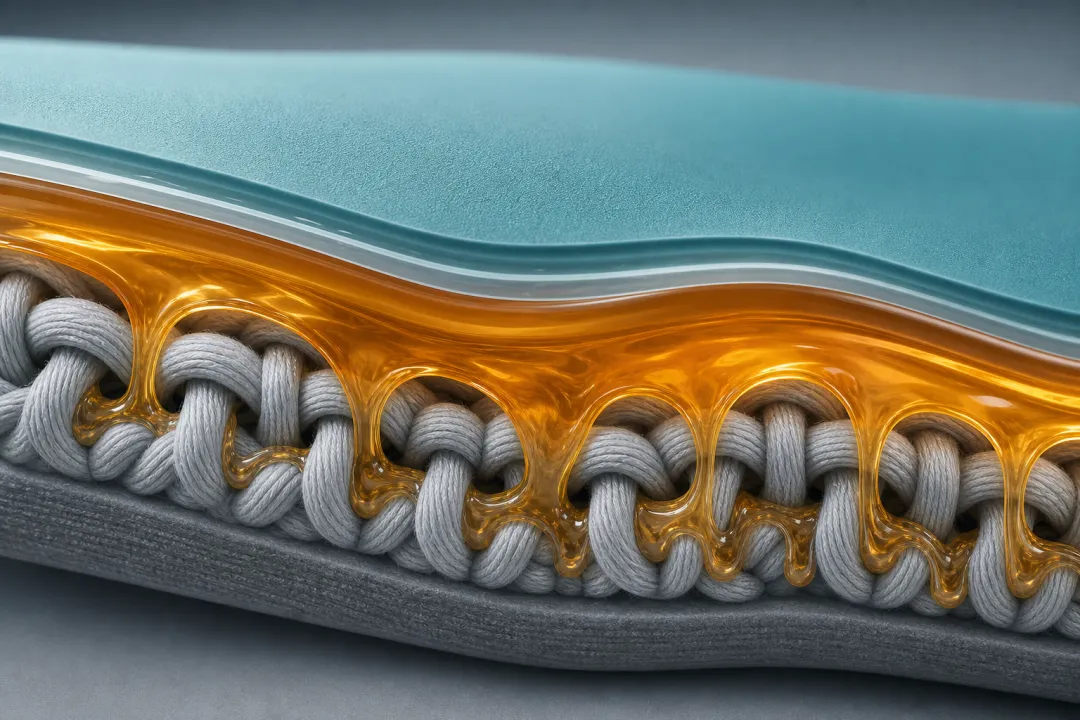
高低温 TPU 膜的破局之道:在微观上实现“一膜分饰两角”!
高低温 TPU 膜断面结构:
┌────────────────────────────────────────────────────────┐ ◄ 表面层:高温耐磨高回弹 TPU (熔点 160℃~180℃,硬度 85A~95A)
├┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┄┤ ◄ 分子级共挤界面 (同分子主链共聚,零界面脱层隐患)
└────────────────────────────────────────────────────────┘ ◄ 底层:低温高粘热熔流动 TPU (熔点 80℃~110℃,硬度 70A~80A)
| | | |
|---|
| 表层:高温功能层 (High-Temp Skin Layer) | 耐磨、抗刮花、耐高温压烫(不熔化变形)、提供哑光/高光/珠光等丰富视觉外观与细腻触感 | 硬度 85A ~ 95A 熔点 160℃ ~ 185℃ | 高硬度聚醚型或聚酯型 TPU,耐黄变等级达 4.0 级以上,具备优异抗撕裂与拉伸回复率 |
| 底层:低温热熔胶层 (Low-Temp Adhesive Base) | 受热迅速熔融流动,充当“固态热熔胶”,深层锚定渗透进鞋面飞织网布或超纤纤维间隙 | 硬度 70A ~ 80A 熔点 80℃ ~ 110℃ | 低结晶度、宽软化区间的改性聚己内酯/聚酯热熔型 TPU,具有极佳的初粘力与极低熔体粘度 |
东莞市凯立兴新材料科技有限公司采用多层共挤(Multi-layer Co-extrusion)流延工艺,将高温熔体与低温熔体在模头内部于熔融状态下一次性复合。两层之间没有任何传统胶水粘接界面,而是分子链级别的物理互穿网络,从根本上杜绝了高温层与低温层自身的层间剥离隐患!
二、鞋面热压工艺实操 SOP:精准锁定“温度-压力-时间”黄金窗口
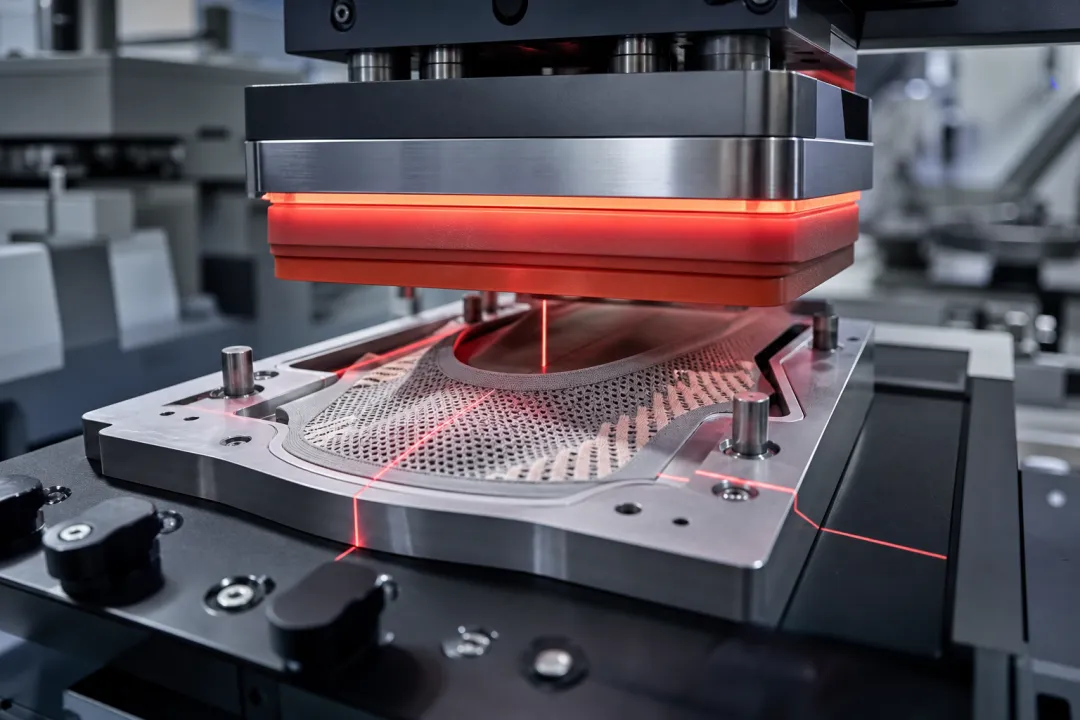
在鞋面热压贴合(Flatbed Heat-Press / High-Frequency Welding)中,操作人员必须将机台参数精准锁定在高低温膜的“差异化熔融窗口”内:
最佳热压操作温度区间:底层低温胶完全熔融活化(≥ 110℃~130℃) < 实际界面温度 < 表层高温层开始软化(≤ 150℃~160℃)
1. 温度控制(Temperature Control)
平板热压机推荐设定
:上模温度 125℃ ~ 145℃,下模常温或微热(约 40℃~60℃);
参数控制核心
:热压瞬间,底层的低温胶层已完全变成流动态液体并深入布料缝隙;而表层的高温层仍处于坚韧的高弹态,完美保留裁片形状与表面纹理,不粘模、不溢焦。
2. 压力设定(Pressure Profile)
推荐气缸工作压力
:3.0 ~ 5.5 kg/cm²(约 0.3 ~ 0.55 MPa);
避坑细节
:压力过小会导致胶水无法挤入致密的飞织布网孔,形成“假粘”;压力过大则会导致低温熔融胶水被过度挤出裁片边缘,形成毛刺状的“溢胶(Glue Overflow)”。
3. 热压停留时间与冷压定型(Dwell Time & Cold Pressing)
热压时间
:通常控制在8 ~ 15 秒(厚织物或多层补强片适当延长至 18 秒);
冷压关键步(至关重要)
:热压完成后,必须立即移入冷压工位(带有循环冷却水的压机,温度 ≤ 20℃,压力 34 kg/cm²)加压冷却 610 秒!
三、鞋厂大货量产的 3 大高发痛点与避坑对策
痛点 1:裁片边缘“溢胶”严重,弄脏鞋面或粘住离型纸
根因剖析
:① 热压温度过高(如超过 155℃)导致低温胶层流动性过大;② 底层胶层厚度占比过大;③ 压力过猛。
解决思路
:
痛点 2:水洗或反复弯折后“边缘起翘脱层”
根因剖析
:① 织物表面残留了过量的防水剂或硅油柔软剂;② 热压时间不足,胶层未完全浸润。
解决思路
:
痛点 3:深色膜贴在浅色鞋面上发生“耐黄变失效与色迁移”
根因剖析
:选用了耐黄变等级仅 2~3 级的低端芳香族 TPU,在日光紫外线照射下泛黄变色;或染料发生分子间热迁移。
解决思路
:
四、鞋材成品出厂 3 项严苛力学测试标准
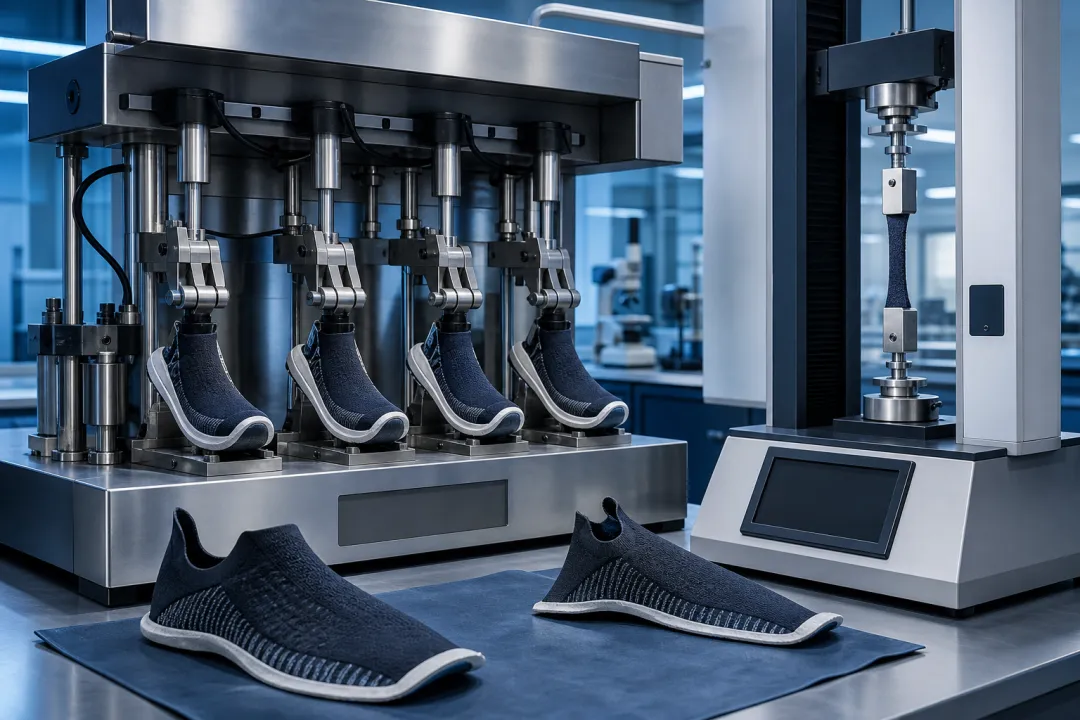
为了确保大货鞋款达到一线品牌商的验收标准,东莞市凯立兴新材料科技有限公司建议代工厂必须通过以下 3 项质检测试:
| | |
|---|
| 1. 鞋面曲折耐久测试 (Vamp Flexing Test) | SATRA TM92 / ISO 17707,在鞋面曲折试验机上连续弯折 100,000 次 | TPU 贴合裁片与飞织基材边缘无任何脱开、起翘、裂纹或白化 |
| 2. 剥离强度测试 (Peel Adhesion Strength) | ASTM D903 / SATRA TM401,以 100 mm/min 进行 180° 恒速剥离拉伸 | 剥离力要求 ≥ 30 ~ 50 N/2.5cm,或达到鞋面织物纤维彻底撕裂破坏 |
| 3. 耐反复水洗与汗液浸渍测试 (Wash & Sweat Fastness) | ISO 6330,40℃ 标准家用洗衣机连续机洗 10 次,配合人工酸性汗液浸泡 24h | 表面无气泡发软、无变色,剥离力衰减率控制在 ≤ 10% 以内 |
结语:科技赋能无缝鞋材,让每一双跑鞋兼具颜值与实力
从传统厚重车缝到极致轻量热贴,高低温双层共挤 TPU 薄膜不仅重塑了现代运动鞋的工业美学,更大幅提升了鞋厂的自动化生产效率与产品良率。
东莞市凯立兴新材料科技有限公司依托高分子共挤流延核心技术与全自动化精密涂布线,为全球鞋业品牌与代工厂提供从0.15mm~0.60mm 各类厚度配比、哑光/镜面/幻彩纹理到全脂肪族耐黄变高低温 TPU 膜的全套应用解决方案,并提供专业打样及热压工艺窗口参数调优服务。
手头有运动鞋、飞织鞋面补强或越野跑鞋新项目需要高低温 TPU 膜打样测试?欢迎添加微信 18820723050,可申请寄送精准匹配的样品并免费领取《TPU 薄膜选型手册》完整版电子书。
How to Select High-Low Temperature Co-Extruded TPU Film for Seamless Footwear: Principles and Heat-Press Processing Guide
Column: Product Application & Manufacturing Process | By Dongguan Kailixing New Material Technology Co.,LTD (TPU film factory) Note: This article provides engineering methodologies regarding the structure, thermal bonding, and defect prevention of high-low temperature co-extruded TPU films in seamless athletic footwear uppers. Specific layer thickness ratios, press temperatures, and peeling adhesion targets should refer to formal project Technical Data Sheets (TDS) and prototype trials.
Introduction: From Stitching Lines to Seamless Lamination — The Footwear Revolution
Inside modern athletic footwear factories, conventional stitch-and-sew assembly lines are rapidly giving way to automated CNC cutting, high-frequency welding, and automated heat-press stations.
On modern running shoes, soccer cleats, basketball footwear, and trail runners, bulky stitched synthetic leathers have been replaced by ultra-sleek, lightweight, and durableSeamless No-Sew Uppers.
The cornerstone material enabling this engineering transformation is theHigh-Low Temperature Co-extruded TPU Film.
Footwear manufacturers frequently face trial hurdles:
Why do single-layer TPU films melt entirely and stick to press plates?
Why do certain multi-layer films exhibit severe glue overflow along die-cut edges?
Why do toe-box flex zones peel and delaminate after 20,000 bending cycles?
Dongguan Kailixing New Material Technology Co.,LTD explains the dual-layer co-extrusion architecture, parameter optimization, and failure prevention.
1. Material Architecture: What Is High-Low Temperature Co-Extruded TPU Film?
Single-layer films cannot simultaneously satisfy structural surface requirements and thermal melt bonding:
Low-Melting-Point Hot-Melt Film (80°C–100°C)
melts completely into liquid glue, destroying surface cosmetics and contaminating press platens.
High-Melting-Point TPU Film (160°C–180°C)
provides surface durability but cannot soften at fabric-safe temperatures, leading to bond failure.
High-Low Temperature Co-extruded TPU solves this by integrating dual functional domains:
Top High-Temperature Skin Layer (0.05–0.30 mm / 85A–95A / Tm 160°C–185°C)
:
Bottom Low-Temperature Hot-Melt Adhesive Layer (0.03–0.15 mm / 70A–80A / Tm 80°C–110°C)
:
Dongguan Kailixing New Material Technology Co.,LTD utilizesmulti-layer co-extrusion casting technology, fusing both layers in the molten phase to achieve molecular-level entanglement, permanently eliminating interlaminar delamination risks.
2. Flatbed Heat-Press Operating SOP: Calibrating the Golden Window
The target operating window is:Adhesive base fully activated (≥110°C–130°C) < True Interface Temp < Skin layer begins softening (≤150°C–160°C).
Temperature Profile
: Top platen set to125°C–145°C, bottom bed at room temperature or warm (40°C–60°C).
Pneumatic Pressure
: Maintained at3.0–5.5 kg/cm² (0.3–0.55 MPa). Insufficient pressure causes cold-bonding voids; excessive pressure squeezes molten adhesive out of die-cut perimeters.
Dwell Time & Cold Pressing
: Hot press for8–15 seconds, followed immediately by transfer to awater-cooled chiller press (≤20°C, 3–4 kg/cm²) for 6–10 secondsto crystallize the adhesive and lock bond strength.
3. Footwear Manufacturing Troubleshooting & Preventive Strategies
Edge Glue Overflow & Flashing
:
Post-Wash Edge Peeling & Flex Delamination
:
Yellowing and Color Bleed on Light-Colored Shoes
:
4. Laboratory Acceptance and Qualification Testing
Footwear Vamp Flex Endurance (SATRA TM92 / ISO 17707)
: 100,000 continuous flex cycles with zero edge lifting, micro-cracking, or chalking.
180° Peel Adhesion Strength (ASTM D903 / SATRA TM401)
: Peel force reaching≥30–50 N/2.5cmor substrate fiber-tear.
Wash and Perspiration Fastness (ISO 6330)
: Zero bubbling or discoloration after 10 standard machine washes and 24h acidic sweat immersion.
Conclusion: Engineering Excellence in Seamless Footwear
From traditional stitching to lightweight thermal lamination, high-low temperature co-extruded TPU films drive productivity and futuristic aesthetics in modern footwear.
Dongguan Kailixing New Material Technology Co.,LTD supplies custom gauges (0.15mm–0.60mm), aliphatic anti-yellowing formulations, and comprehensive process matching support.
For technical data sheets, sample swatch books, or heat-press process consulting, contact WeChat / Phone: +86 18820723050.